

Medical Injection Molding: Prototype & Pilot Production Guide
Introduction
Medical product development often requires more than a visual prototype. Housings, connectors, cartridges, instrument components and internal structural parts may need to be evaluated for assembly, strength, dimensional stability, chemical resistance and production repeatability. Medical injection molding at the prototype and pilot stage allows teams to test parts made from the intended thermoplastic before investing in full production tooling. HPDI’s prototype and low-volume molding services are applicable to development programs where production-like parts are required for engineering verification.
Medical Injection Molding Development Stages
| Development Stage | Main Goal | Typical Output |
|---|---|---|
| Concept prototype | Confirm form and basic fit | 3D printed / machined parts |
| Prototype injection molding | Validate resin and molded behavior | Production-like molded samples |
| Pilot production | Evaluate repeatability and assembly | Small controlled batch |
| Production tooling | Scale stable design | Qualified production parts |
1. Define the Part’s Intended Use and Risk
Before selecting a resin or mold structure, document how the part will be used. Does it contact a patient, fluid, reagent or medication? Is it reusable or disposable? Will it be sterilized or repeatedly cleaned? Is the component load-bearing, cosmetic, transparent or part of a sealed assembly? These questions affect material selection, tolerance, surface requirements and validation planning. Regulatory requirements should be defined by the device manufacturer and quality system for the specific application.
2. Select Materials for the Real Environment
Medical plastics may be chosen for impact resistance, transparency, chemical compatibility, dimensional stability, temperature resistance or sterilization performance. PP, PC, ABS, PC-ABS, POM, TPE and high-performance engineering resins can each be appropriate in different applications. There is no universal ‘medical plastic.’ The selected grade, additives, colorants and supplier documentation need to match the device’s intended use and validation plan.
3. Use DFM to Protect Cleanability and Function
Design for manufacturability should review wall thickness, draft, ribs, bosses, weld lines, gate location, ejector marks and parting lines. For medical equipment, it can also be important to avoid unnecessary crevices or features that complicate cleaning and assembly. A gate mark that is acceptable inside a housing may be unsuitable on a sealing surface. Critical dimensions should be clearly identified so that the mold maker can focus process control and inspection where it matters most.
4. Prototype Tooling Provides Production-Like Evidence
A prototype mold can be built with a simplified structure while still using the intended production resin and an injection molding machine. This allows engineers to study shrinkage, warpage, assembly force, screw-boss strength, snap-fit behavior and molded surface quality. The case study page explains how molded prototypes are used to detect process or material problems before mass production.
5. Pilot Production Tests More Than the Part
A few molded samples may validate geometry, but a pilot batch can reveal process variation, assembly yield, handling issues, packaging damage and inspection bottlenecks. This is important before a production mold is multiplied to more cavities or integrated with automation. Pilot quantities can also support internal engineering builds, field evaluation or other product-specific verification activities defined by the manufacturer.
6. Inspection Should Focus on Critical-to-Quality Features
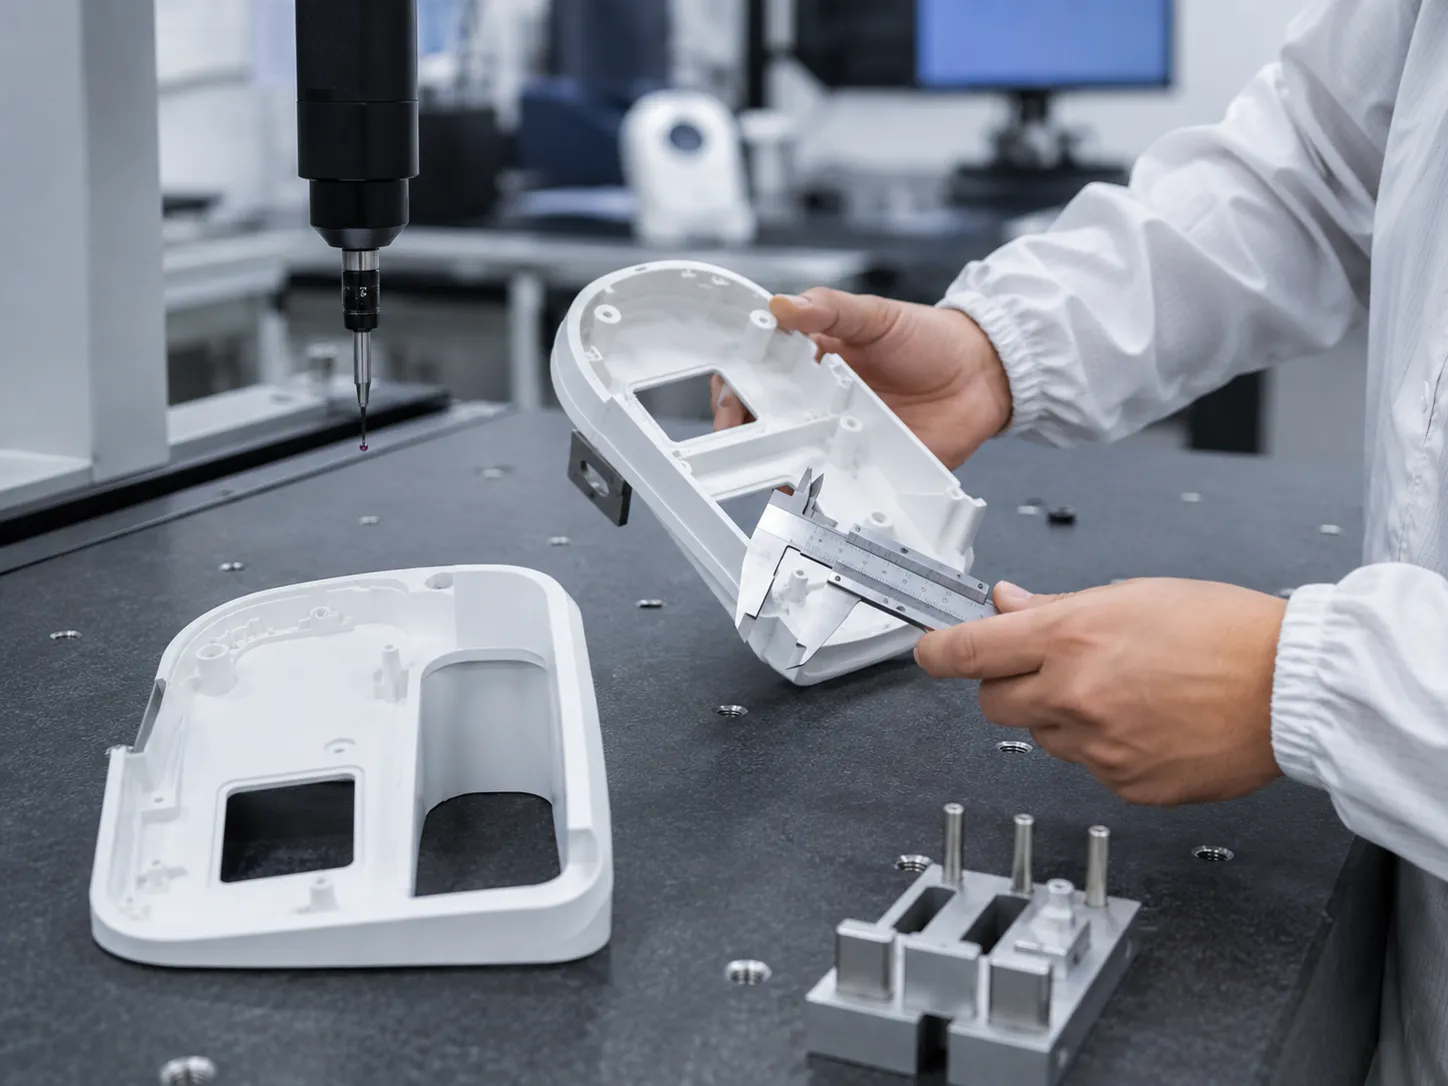
Medical components often have dimensions that matter more than others: sealing surfaces, mating features, sensor positions, wall interfaces or alignment references. A practical inspection plan separates critical dimensions from reference dimensions. Dimensional reports, visual standards and functional gauges can then be matched to risk. HPDI’s facilities page shows its mold manufacturing, molding and dimensional measurement resources for prototype and low-volume work.
7. Maintain Traceability During Development
Even before formal mass production, it is useful to keep clear records of CAD revisions, resin grades, mold changes, process settings and sample approvals. This helps engineering teams understand why one build differs from another and allows validated learning to transfer into the production mold. The FAQ outlines information used for quotations and project planning, while the contact page provides a direct route for submitting project requirements.
Additional Planning Consideration
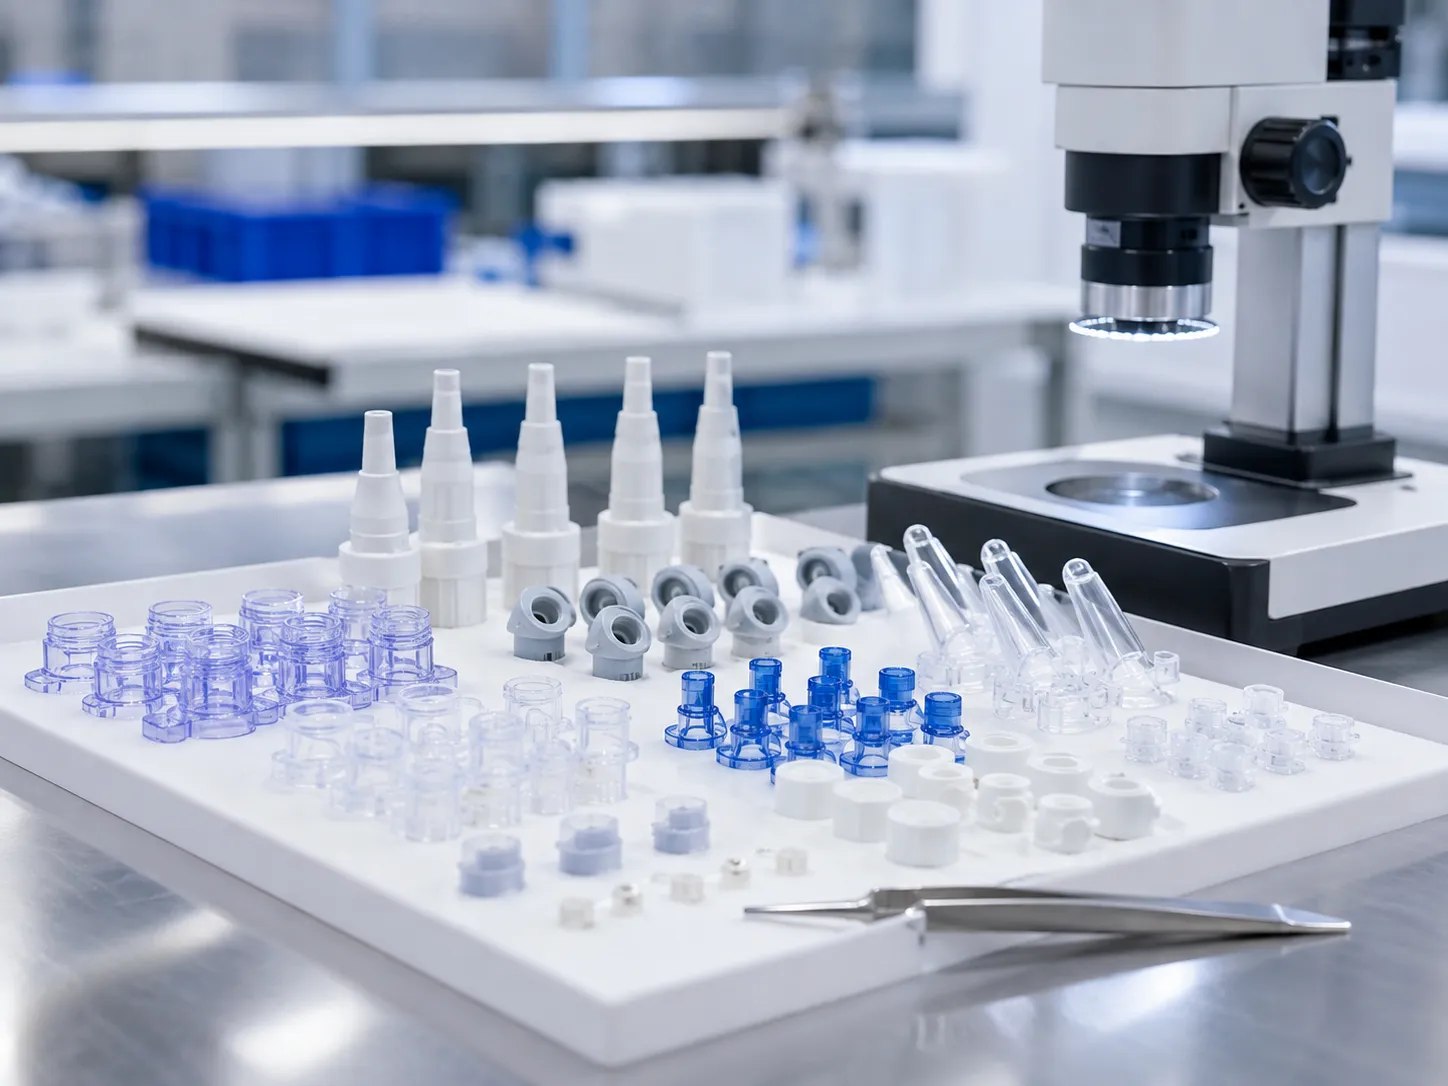
For medical development, communication between product engineering, quality and the mold supplier should begin early. The mold maker needs to know which dimensions and surfaces are critical, while the quality team needs to know what the prototype process can and cannot prove. Aligning these expectations prevents a prototype batch from being treated as formal qualification when it was intended only for engineering learning.
Practical Project Tip
Before tooling approval, hold a short review with design, manufacturing, quality and purchasing. Confirm the drawing revision, resin, quantities, critical dimensions, cosmetic requirements, expected tool life and approval process. This simple cross-functional check prevents many quotation and tooling changes caused by different teams working from different assumptions.
Additional Validation Note
Pilot planning should also define how nonconforming parts will be handled. Even a development batch benefits from simple rules for segregation, reinspection and disposition. This prevents questionable samples from entering engineering tests and gives the mold team clearer feedback about recurring defects. The same discipline makes it easier to transfer lessons from the prototype tool into the later production quality plan.
Conclusion
Medical injection molding for prototype and pilot production is most valuable when it is treated as a structured engineering stage rather than simply a way to obtain samples. Material selection, DFM, prototype tooling, controlled molding, inspection and pilot builds work together to identify risks before production scale increases. The result is a stronger handoff from design verification to stable manufacturing, with fewer surprises after the final tool has been committed.